Leave Your Message
High-performance replacement battery solutions designed to meet the rigorous demands of retail and payment environments.
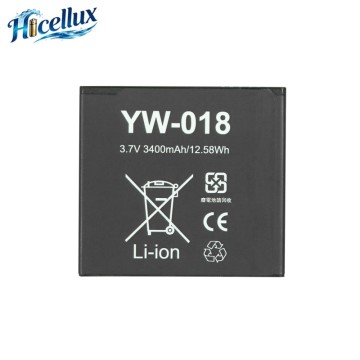 Lenovo Thinkpad POS Compatible Terminal Battery - PAX YW-018 D230 Replacement (3.7V 3400mAh)
 Lenovo Thinkpad Standard POS Power - Verifone VX520 VX520C VX670 Replacement (7.4V 1800mAh)
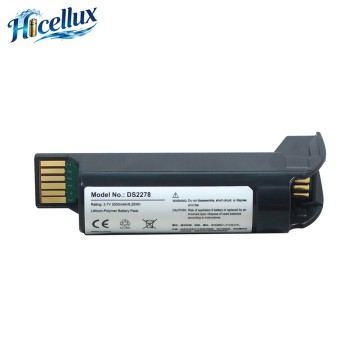 Lenovo Thinkpad Grade Scanner Battery - Zebra DS2278 BT-000317-01 Replacement (3.7V 2500mAh)
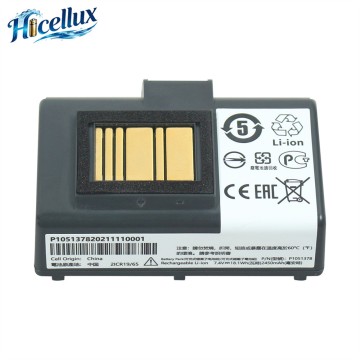 Lenovo Thinkpad Compatible Mobile Printer Battery - Zebra QLN320 QLN220 ZQ520 Replacement (7.2V 2600mAh)
The global retail and financial services landscapes are undergoing a rapid paradigm shift. Traditional checkout lanes with stationary cash registers are quickly being replaced or supplemented by versatile Mobile Point of Sale (mPOS) terminals, smart kiosks, and handheld scanning devices. In this highly dynamic environment, the demand for uninterrupted, high-capacity, and long-lasting portable power is critical. The integration of Lenovo Thinkpad battery standards into retail and payment POS terminals represents a major technological convergence, bringing enterprise-grade laptop reliability, safety, and longevity to the frontlines of commerce.
Retail operations, hospitality venues, and logistics networks cannot afford system downtime. A dead battery on a POS terminal directly translates to lost sales, frustrated customers, and damaged brand reputation. To combat this, hardware developers and replacement battery manufacturers are leveraging the advanced lithium-ion and lithium-polymer technologies originally perfected for high-drain enterprise laptops, such as the Lenovo Thinkpad series. These batteries deliver the stable voltage, rapid charging capabilities, and advanced thermal management required to keep modern transactional systems running smoothly through consecutive shifts.
Unlike standard consumer-grade batteries, industrial-grade battery solutions compatible with Lenovo Thinkpad and leading POS terminal brands are engineered to withstand continuous charge-discharge cycles, extreme temperature fluctuations, and physical drops. They feature intelligent Battery Management Systems (BMS) that protect against overcharging, deep discharging, and short-circuiting, ensuring maximum safety in crowded retail environments.
Today's retail and payment terminals are far more than simple card readers; they are sophisticated edge-computing devices. Powered by advanced operating systems, large color touchscreens, thermal printers, barcode scanners, and multiple wireless radios (Wi-Fi, Bluetooth, 4G/5G LTE), their power consumption has skyrocketed. Consequently, legacy battery technologies are no longer sufficient.
The market is seeing a massive surge in demand for high-capacity replacement batteries that match the exact specifications of original equipment manufacturers (OEMs). Business owners are realizing that investing in premium, certified replacement batteries is a highly cost-effective strategy to extend the operational life of their existing POS terminal fleets. By upgrading to high-performance cells, retailers can avoid the capital-intensive process of replacing entire terminal systems, achieving a significantly lower Total Cost of Ownership (TCO).
In busy supermarkets and department stores, mobile cashiers use handheld POS terminals to perform "queue-busting" during peak hours. These terminals must remain active for up to 10-12 hours of continuous scanning, printing, and card processing. A battery utilizing Lenovo Thinkpad-grade cells ensures that the voltage does not drop even during power-intensive tasks like printing a thermal receipt or activating a high-power laser scanner.
Restaurants, bars, and cafes rely heavily on wireless payment terminals brought directly to the customer's table. These devices are frequently exposed to spills, drops, and constant docking/undocking. Batteries designed with robust internal packaging and secure contact pins prevent power interruptions caused by physical vibration and minor impacts.
Courier services and field technicians require rugged handheld terminals (like Zebra and Honeywell devices) to verify deliveries and accept payments on the spot. These terminals operate in extreme environments—from freezing winter temperatures to hot summer delivery vans. Superior thermal stability, a hallmark of Thinkpad battery engineering, ensures consistent energy output regardless of external weather conditions.
To understand why these batteries perform so reliably, it is essential to examine their internal components. A premium replacement battery consists of A-grade lithium-ion cells, a precision-engineered printed circuit board (PCB), and a flame-retardant outer shell. The PCB acts as the brain, constantly monitoring voltage levels of individual cells to ensure balanced charging. This prevents localized overheating, which is the primary cause of battery swelling and premature degradation. By adhering to the strict manufacturing standards utilized in enterprise laptop batteries, our POS replacement batteries deliver unmatched reliability and safety.
We provide one-on-one customized services and cost-effective solutions for our global clients.


Building a sustainable future through innovation, customer-centricity, and absolute integrity.
To be the world's most trusted partner in portable energy solutions, driving the future of smart retail and terminal connectivity.
To empower businesses globally by delivering high-quality, safe, and cost-effective battery technologies that maximize uptime and profitability.
• Customer First • Innovation as Our Core • Integrity as Our Foundation • Collaboration & Responsibility
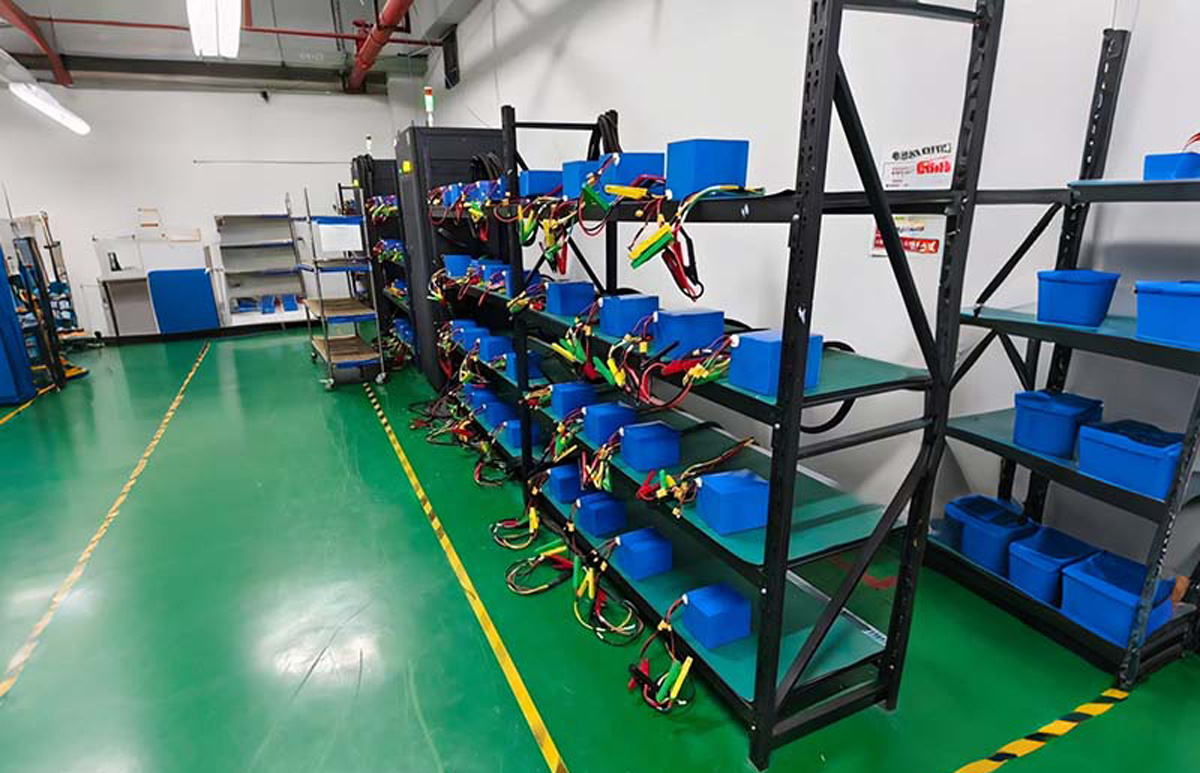
Take a closer look at our advanced manufacturing lines and quality assurance processes.
Our factory operates fully automated production lines tailored to battery manufacturing, covering the entire process from initial material input to finished product packaging, ensuring consistency and speed.
Equipped with industry-leading technology including automatic cell sorting machines, robotic spot-welding systems, and PCB precision processing workshops that cut manual intervention by 80%.
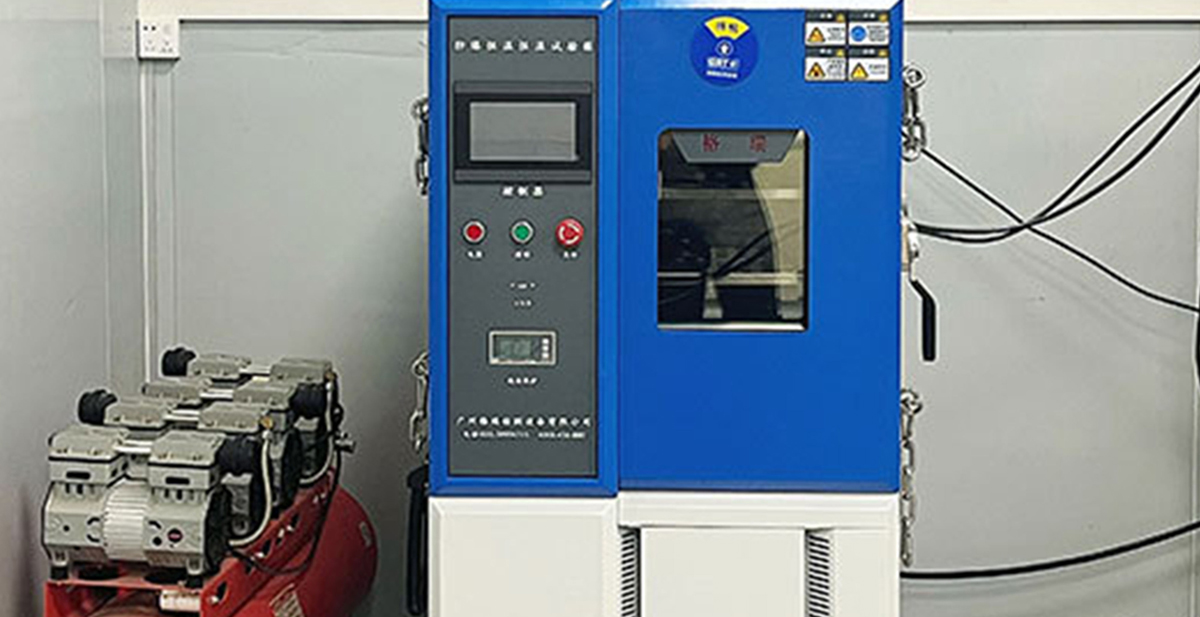
Our 70+ professional quality control team monitors every stage: from incoming material verification to 100% coverage of aging tests and real-time performance detection.
A decade of deep integration, research, and global service excellence.
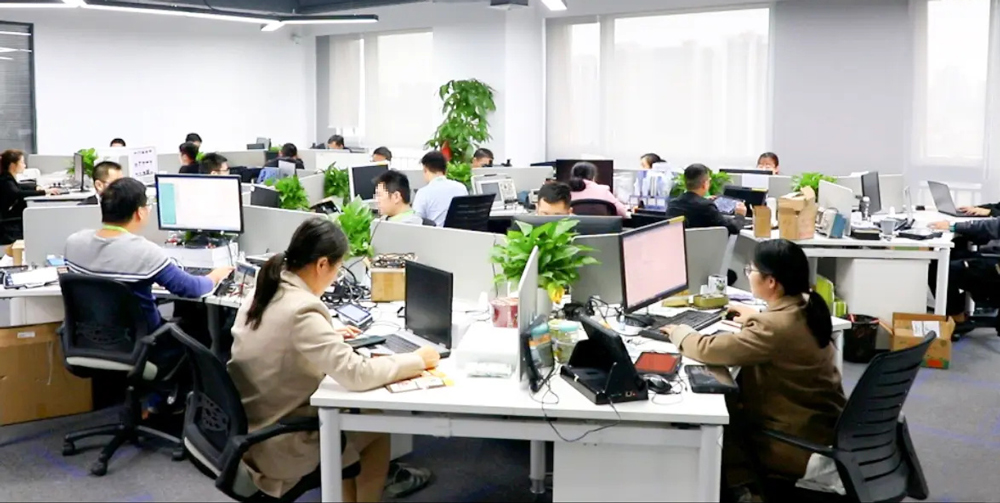
Our group has been deeply involved in the battery industry for over a decade. We have accumulated profound industry knowledge and are always committed to technological innovation and quality improvement.
With senior engineers and technical experts, we handle the entire process from custom cell configuration and PCB design to mass production, ensuring stable product quality and high performance.
We have established a comprehensive marketing network to accurately grasp market trends and provide customized solutions. Our after-sales team responds quickly to customer needs, providing timely technical support.
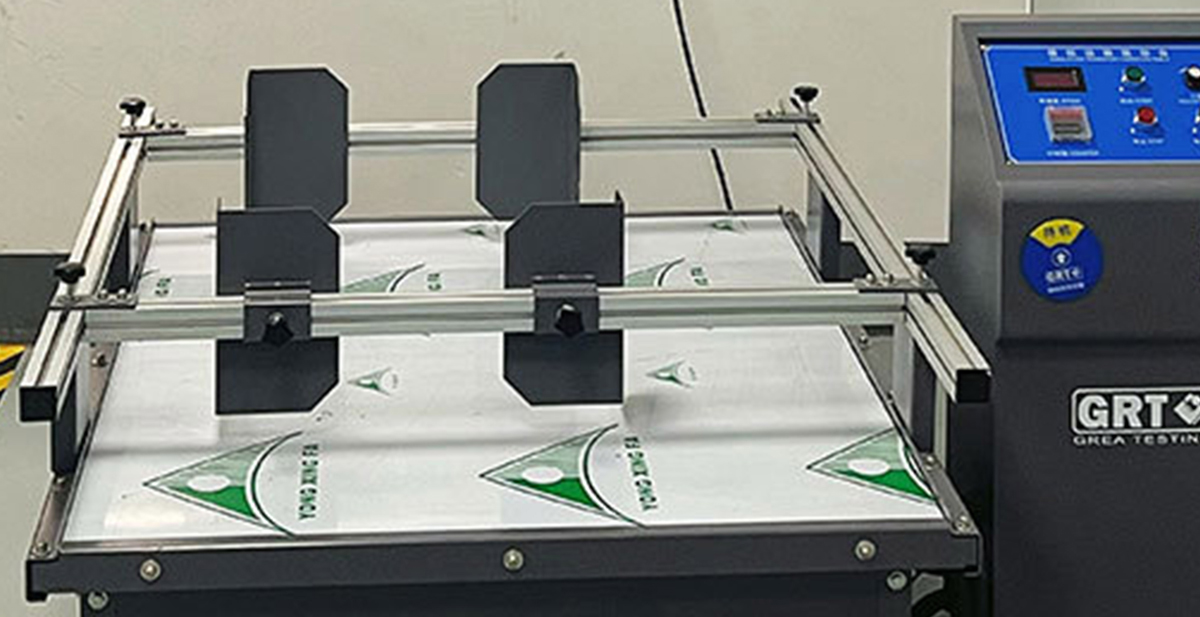
Our products meet the highest safety and environmental standards, including CE, FCC, RoHS, MSDS, UN38.3, and PSE.
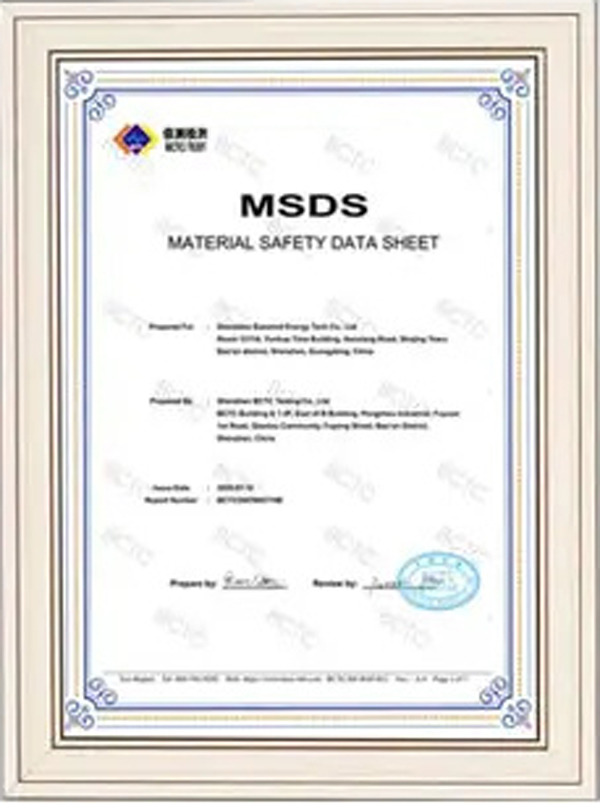
MSDS
FCC
CE
RoHS
Explore our full range of enterprise-grade replacement batteries for laptops, POS terminals, and mobile devices.
Lenovo Thinkpad POS Compatible Terminal Battery - PAX YW-018 D230 Replacement (3.7V 3400mAh)
Lenovo Thinkpad Standard POS Power - Verifone VX520 VX520C VX670 Replacement (7.4V 1800mAh)
Lenovo Thinkpad Grade Scanner Battery - Zebra DS2278 BT-000317-01 Replacement (3.7V 2500mAh)
Lenovo Thinkpad Compatible Mobile Printer Battery - Zebra QLN320 QLN220 ZQ520 Replacement (7.2V 2600mAh)
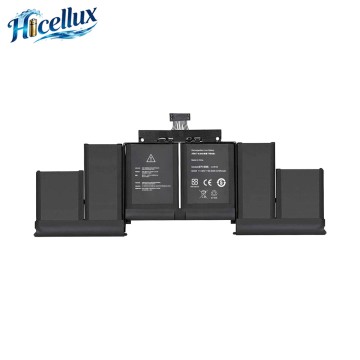 Lenovo Thinkpad Grade Laptop Battery - Apple 99.5WH A1618 Replacement (11.36V 8755mAh)
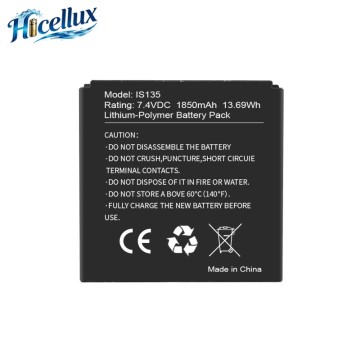 Lenovo Thinkpad Compatible PIN Pad Battery - PAX IS135 Replacement (7.4V 1850mAh)
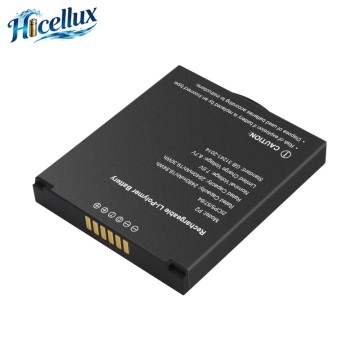 Lenovo Thinkpad Grade Smart POS Battery - Sunmi P2 Replacement (7.6V 2540mAh)
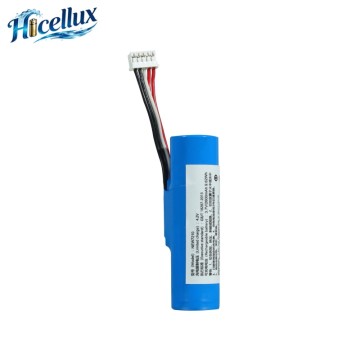 Lenovo Thinkpad Grade Wireless POS Battery - NEWPOS NEW7210 IS588 Replacement (3.7V 2600mAh)