Leave Your Message
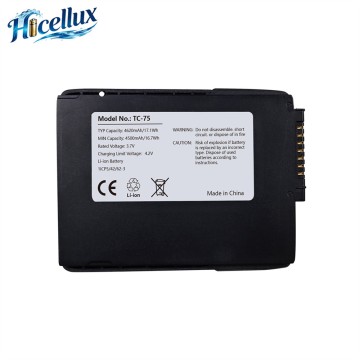
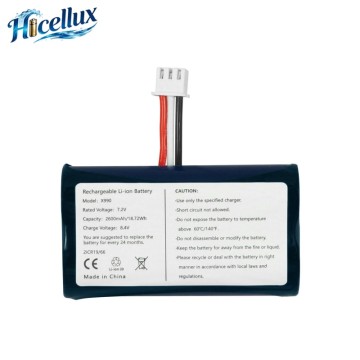
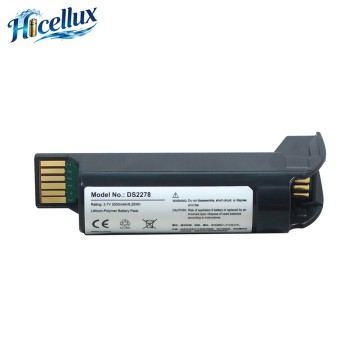
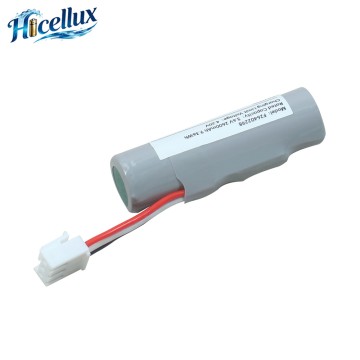
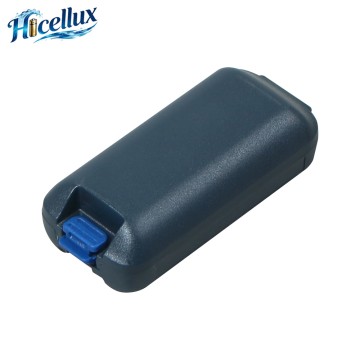
In the rapidly changing world of warehousing, logistics, and supply chain management, operational efficiency is directly tied to the reliability of handheld data collection terminals. Personal Digital Assistants (PDAs) and barcode scanners are the lifelines of modern distribution hubs, processing millions of inventory units daily. To keep these systems running without interruption, there is a growing demand for high-performance battery replacements. The integration of Lenovo Thinkpad-grade battery technology into warehousing and logistics PDA scanners represents a major advancement in industrial mobile power solutions.
Known for their durability, long cycle life, and smart power management, Lenovo Thinkpad battery architectures are now inspiring the design of replacement batteries for industrial scanners. Warehouses operate on tight schedules where even a few minutes of downtime can disrupt the entire supply chain. By utilizing high-density cells, advanced safety circuits, and rugged outer casings, these batteries provide the long-lasting performance required for continuous multi-shift operations.
Unlike consumer electronics, industrial PDA scanners face harsh environments, including extreme temperatures, drops onto concrete, and constant charging cycles. Adapting battery technologies built for high-performance laptops like the Lenovo Thinkpad ensures that mobile terminals have the power capacity and structural integrity to survive demanding daily use.
The logistics sector is undergoing a massive digital transformation driven by e-commerce, global trade, and the need for real-time tracking. This shift has changed how mobile devices are used in warehouses:
Modern fulfillment centers run 24/7. Workers cannot afford to wait for a scanner to charge. Batteries must either last a full 10-to-12-hour shift on a single charge or support hot-swapping—where the battery is replaced without losing data or network connection. High-capacity cells with low internal resistance are crucial to meeting these demands.
Modern logistics managers rely on data to run their operations. Smart batteries equipped with microcontrollers can monitor state-of-health (SoH), count cycles, and track temperature. This allows IT and facility managers to replace aging batteries before they fail, preventing unexpected downtime on the warehouse floor.
Old battery chemistries have been replaced by advanced Lithium-ion (Li-ion) and Lithium-polymer (Li-Po) cells. These materials offer higher energy density, lighter weight, and better performance in cold environments, making them ideal for modern logistics applications.
Industrial PDA scanners are used in a variety of challenging environments. Understanding these scenarios shows why high-quality battery construction is so important:
Cold chain logistics require workers to operate in temperatures as low as -30°C (-22°F). Standard batteries lose capacity rapidly in these conditions, leading to short runtimes and sudden shutdowns. Specialized replacement batteries feature low-temperature cells and advanced thermal insulation to maintain voltage stability, ensuring scanners remain operational throughout the shift.
In busy cross-docking facilities, scanners are constantly in use. The barcode engine, Bluetooth radio, Wi-Fi connection, and screen backlight drain power quickly. Batteries with capacity ratings of 4500mAh or higher are essential to keep these devices running without frequent recharges.
Delivery drivers use PDAs to scan packages, capture signatures, and navigate via GPS. These devices are exposed to direct sunlight, vibration from vehicles, and outdoor weather. Batteries designed with over-temperature protection and rugged shock-absorbing frames prevent swelling and protect the internal cells from physical damage.


To lead the industrial battery industry by providing highly reliable, advanced power solutions that drive efficiency for warehouses, logistics networks, and mobile enterprises worldwide.
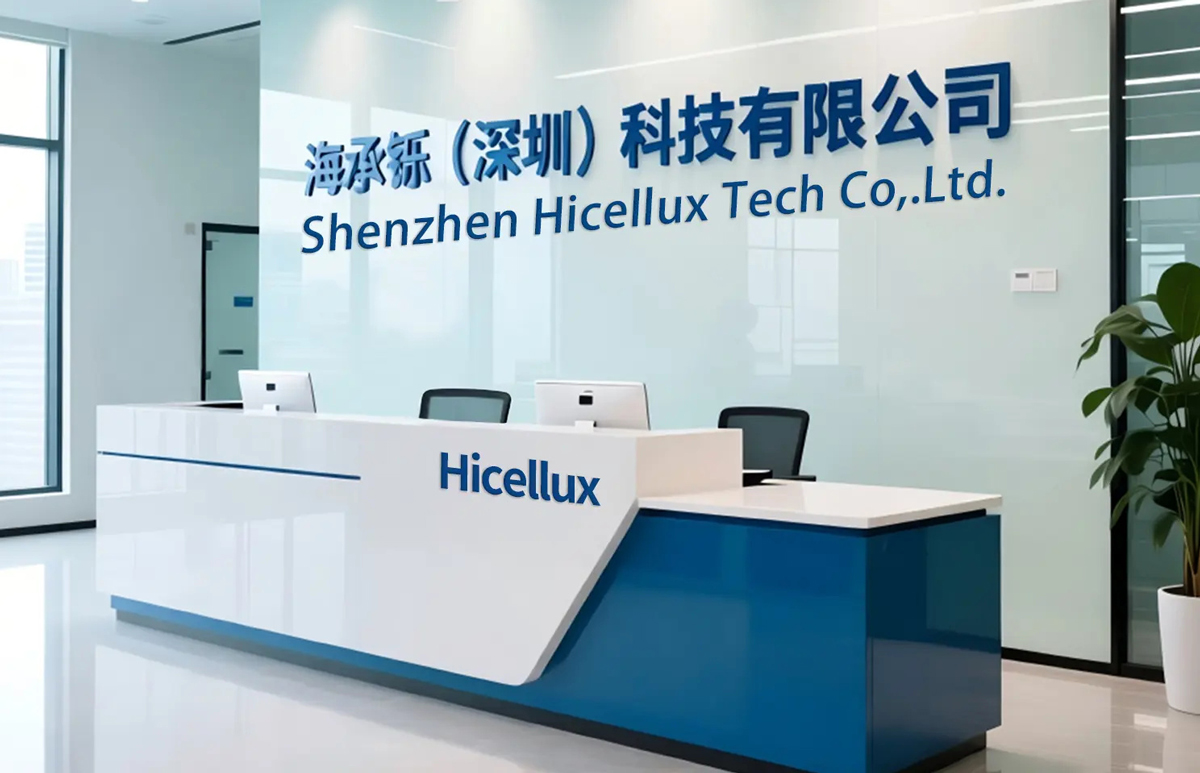
We are committed to delivering high-performance, cost-effective replacement batteries that keep critical business devices running. Through continuous innovation, automated manufacturing, and strict quality control, we help our partners reduce downtime and increase operational profits.
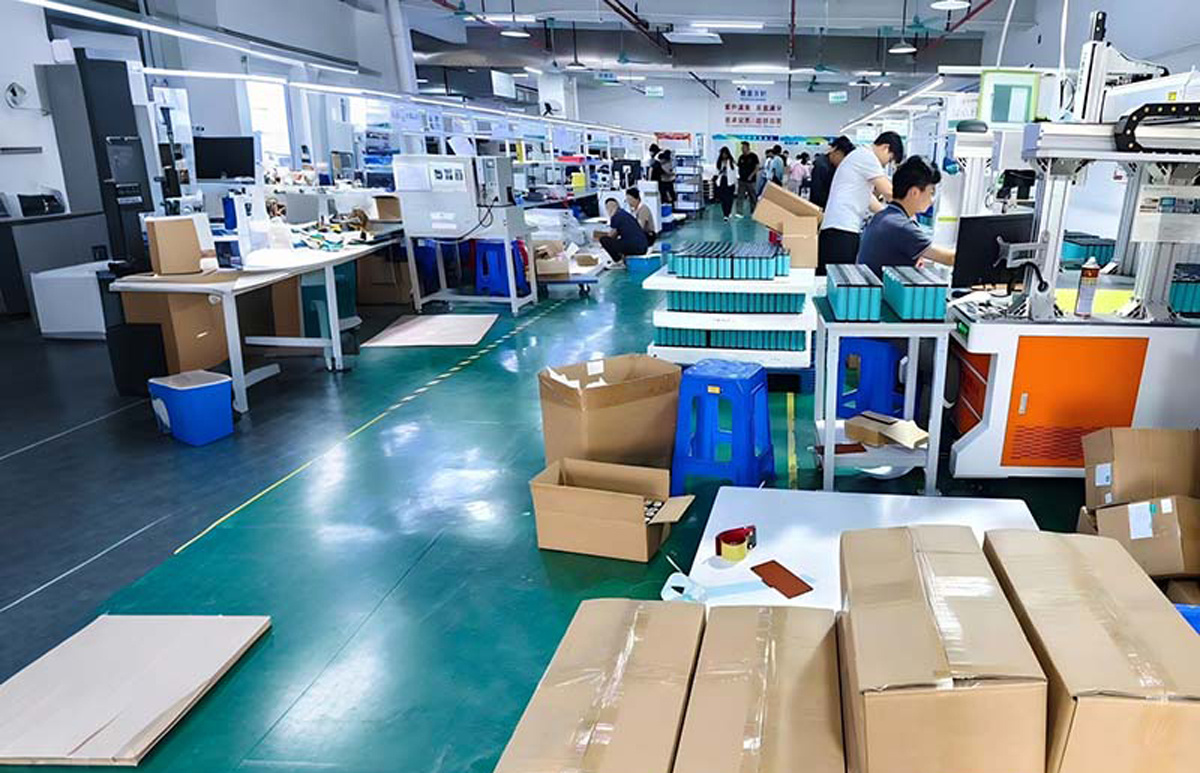
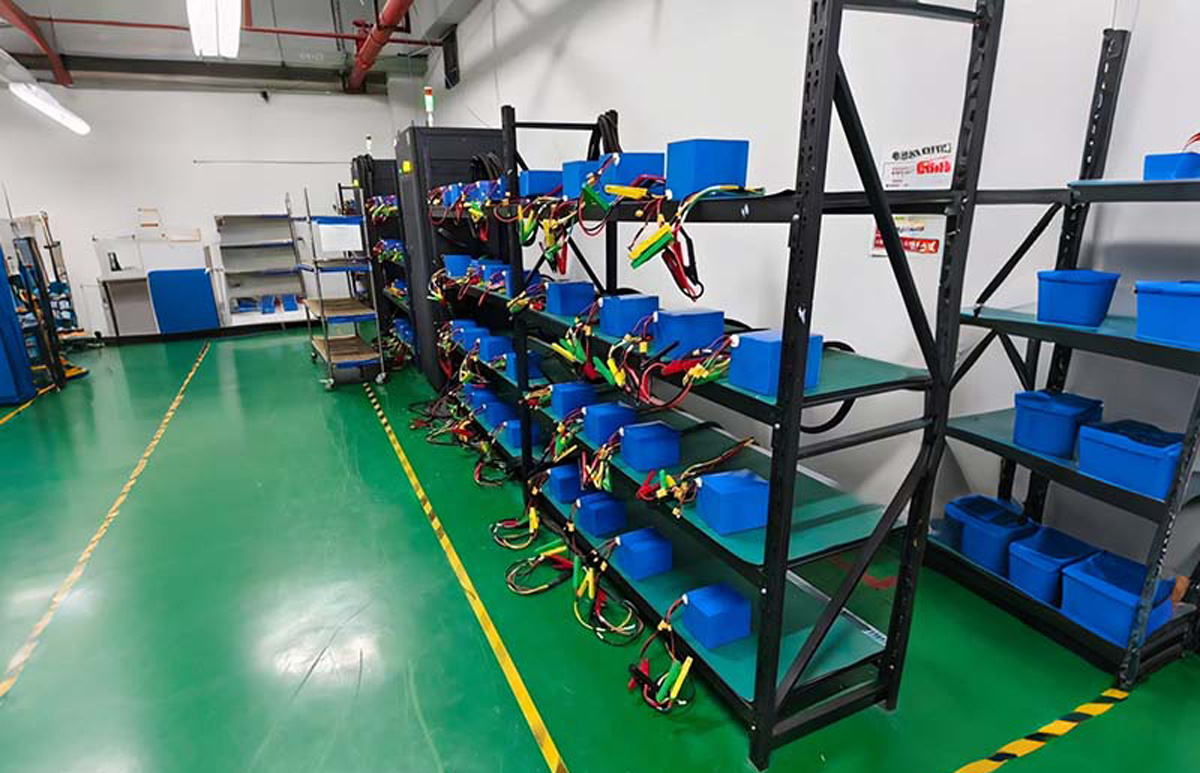
As a professional battery manufacturer, our factory has upgraded a fully automated production line tailored to battery manufacturing, covering the entire process from material input to finished product delivery.
We’re equipped with industry-leading intelligent equipment: automatic cell sorting machines, robotic spot-welding systems, and PCB precision processing workshops—these cut manual intervention by 80% while boosting production efficiency by 60%.
Our 70+ professional team (including automation engineers, quality inspectors, and logistics specialists) monitors every link: from incoming material verification, real-time tracking of cell sorting accuracy, to 100% coverage of aging tests and finished product performance detection.
To understand why replacement batteries inspired by Lenovo Thinkpad standards perform better, it helps to look at their internal components and design features:
A high-quality battery requires a smart management system. The integrated BMS protects the cells from common issues like overcharging, over-discharging, and short circuits. It also balances the individual cells during charging, extending the overall lifespan of the battery pack and ensuring consistent performance over time.
Using premium, A-grade lithium cells ensures the battery maintains its capacity over hundreds of charge cycles. This reduces the frequency of battery replacements, lowering the total cost of ownership for logistics companies.
The outer casing is made from flame-retardant, impact-resistant polycarbonate materials. This rugged design protects the internal cells from drops, vibrations, and physical impacts common in fast-paced warehouse environments.
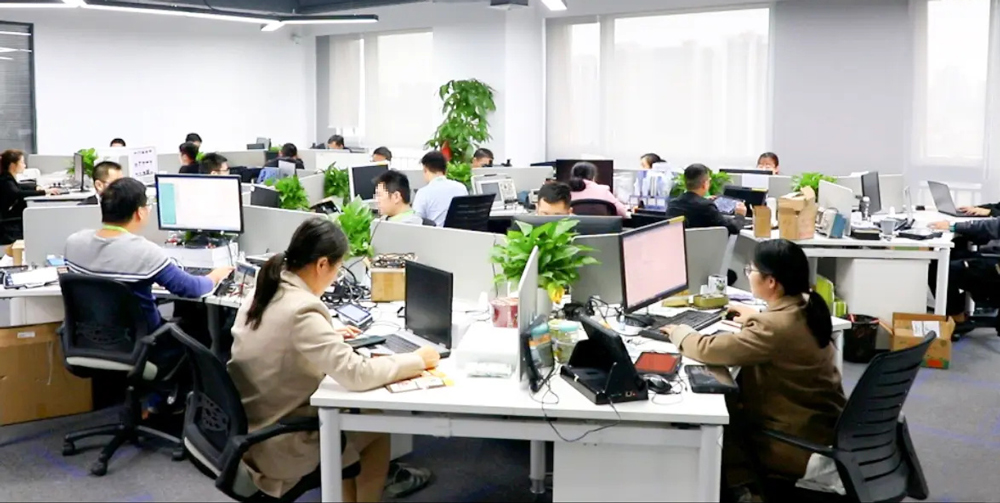
Our team is a professional and experienced group that has been deeply involved in the battery industry for over a decade. We have accumulated profound industry knowledge and are always committed to technological innovation and quality improvement. We have built a strong and integrated capability covering R&D, production, marketing and after-sales service, making us a reliable partner in the battery field.
In terms of R&D and production, we have a team of senior engineers and technical experts with rich experience in battery technology research and product development. Equipped with advanced production equipment and strict quality control systems, we can independently complete the whole process from product design, technology research to mass production, ensuring stable product quality and high performance that meet market demands.
In marketing and after-sales service, we have a professional team with keen market insight and efficient execution. We have established a comprehensive marketing network to accurately grasp market trends and provide customized solutions for customers. Meanwhile, our after-sales team responds quickly to customer needs, providing timely technical support and service guarantee, winning wide recognition and trust from customers. With our all-round strength, we are committed to promoting the development of the battery industry and creating greater value for our partners.
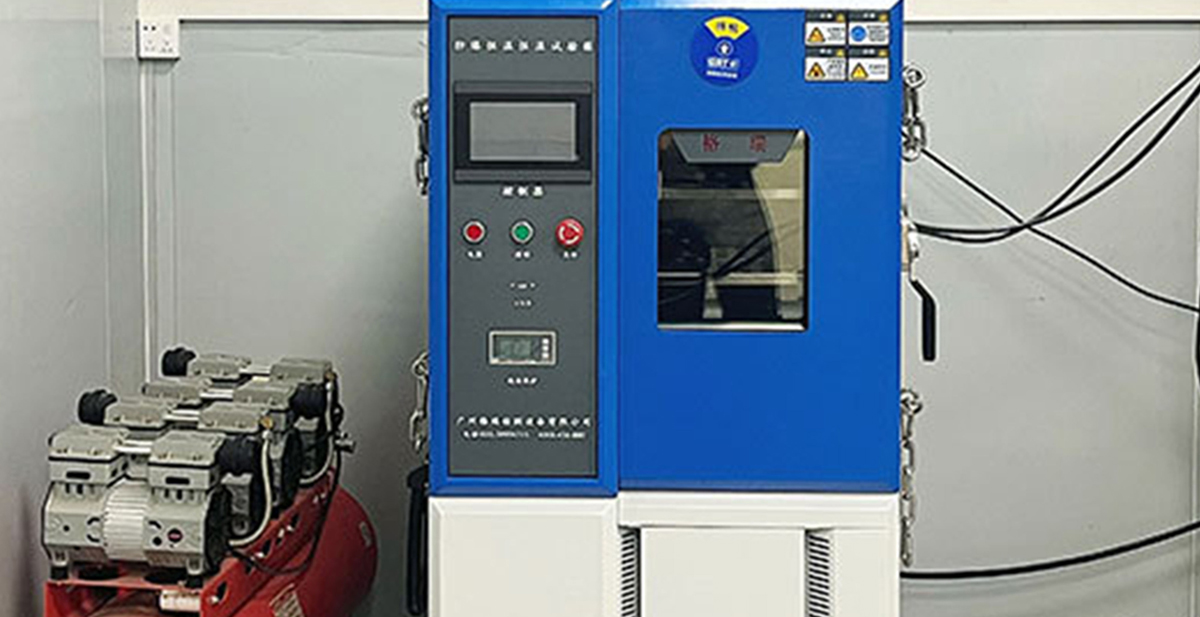
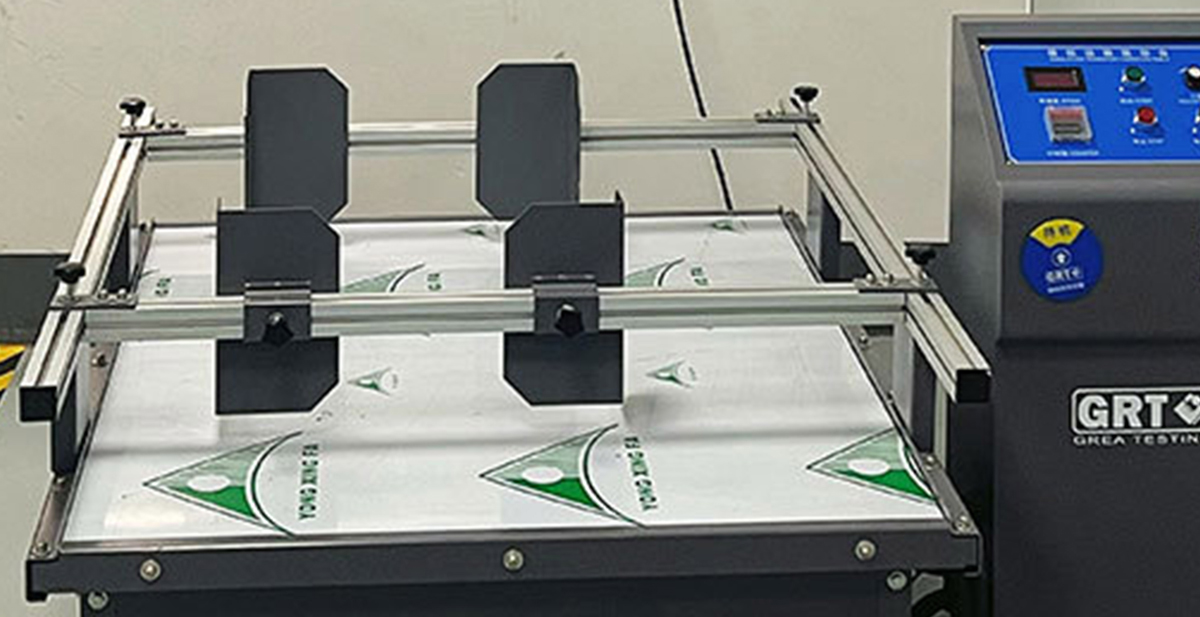
API 6D, API 607, CE, ISO9001, ISO14001, ISO18001, TS. (If you need our certificates, please contact us.)
PSE
UN 38.3
DGM
CE
RoHS
MSDS
FCC
Quality Certified