Leave Your Message
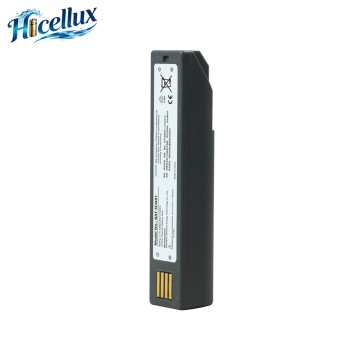
Explore our high-performance replacement batteries engineered to support commercial scanners, mobile printers, and logistics equipment across North America.
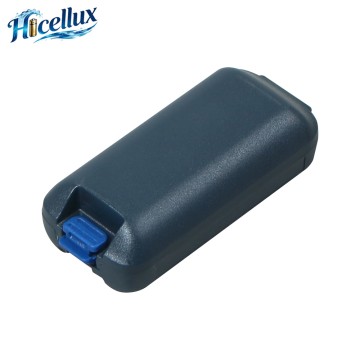
In the United States, enterprise mobility is the backbone of supply chain operations, retail logistics, healthcare tracking, and field service management. Zebra Technologies has established itself as the industry standard for rugged mobile computers, barcode scanners, and thermal barcode printers. Devices like the Zebra TC51, TC52, TC57, TC70, MC3300, and QLn series printers are deployed in thousands of fulfillment centers, distribution hubs, and retail outlets nationwide. However, the performance of these devices is directly bound to their power source. To maintain continuous 24/7 operations, American industries rely heavily on top-tier ODM Zebra replacement battery manufacturers to supply high-performance, cost-effective, and fully compatible power solutions.
Major distribution hubs in California, Texas, and Illinois run continuous shifts where scanner downtime directly impacts delivery SLAs. High-density replacement batteries are crucial for non-stop workflows.
Hospitals and clinics across the US use handheld scanners for medication administration and patient identification. These devices require reliable, medical-grade battery performance.
From frozen food storage in the Midwest to summer heat in Arizona, rugged replacement batteries must withstand extreme temperatures without losing charge capacity.
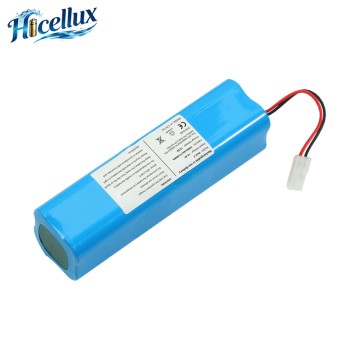
The demand for Zebra replacement batteries in North America is driven by the need for operational efficiency and budget optimization. Original Equipment Manufacturer (OEM) batteries often come with premium price tags, which can significantly inflate the total cost of ownership (TCO) for large fleets of mobile computers. By partnering with a trusted ODM Zebra replacement battery supplier like Hicellus, US enterprises can access customized battery designs that match or exceed OEM specifications in capacity, cycle life, and safety features.
Furthermore, our ODM capabilities allow us to address specific pain points faced by US logistics companies, such as modifying battery management systems (BMS) to support faster charging protocols or integrating smart battery telemetry that communicates battery health directly to mobile device management (MDM) platforms. This level of customization ensures that American businesses can optimize their hardware investments, minimize downtime, and maintain peak productivity.
We provide one-on-one customized services and cost-effective solutions for our clients. Compared to our competitors, we offer faster shipping times and more flexible delivery options. Our company is committed to helping customers improve efficiency and increase profits. We welcome your inquiries and look forward to building long-term, mutually beneficial partnerships with clients worldwide.


Driving the future of portable power through solid corporate values and a clear, client-focused mission.
The industrial battery sector is undergoing a rapid technological evolution. As US companies push for greater automation and faster throughput, the requirements for mobile computer batteries have shifted significantly. The primary focus is no longer just about matching the physical dimensions of the original Zebra battery; it is about maximizing energy density, cycle life, and thermal tolerance.
Modern rugged devices demand more power to run advanced software, high-speed scanning engines, and constant wireless communication (Wi-Fi 6, 5G, Bluetooth). As a leading ODM manufacturer, we utilize premium Grade-A lithium-ion cells that offer higher energy density in the same form factor. This translates to extended shift runs, allowing warehouse operators in the US to complete a full 10-to-12-hour shift on a single charge without needing mid-shift battery swaps.
United States enterprise customers are increasingly deploying Mobile Device Management (MDM) software like SOTI MobiControl or Zebra’s own battery management tools. These tools require batteries equipped with smart fuel gauges (using I2C or HDQ communication protocols) to report real-time health data, including state of charge (SoC), state of health (SoH), temperature, and cycle count. Our ODM replacement batteries are engineered with advanced Smart BMS boards that seamlessly integrate with these systems, allowing fleet managers to proactively replace aging batteries before they fail on the warehouse floor.
Industrial environments in the US are notoriously demanding. Scanners are dropped on concrete, exposed to moisture, and subjected to electrostatic discharge (ESD). Consequently, our replacement batteries feature ultra-rugged polycarbonate housings, gold-plated connection pins to prevent corrosion, and comprehensive safety circuits that protect against overcharging, over-discharging, short circuits, and thermal runaway.
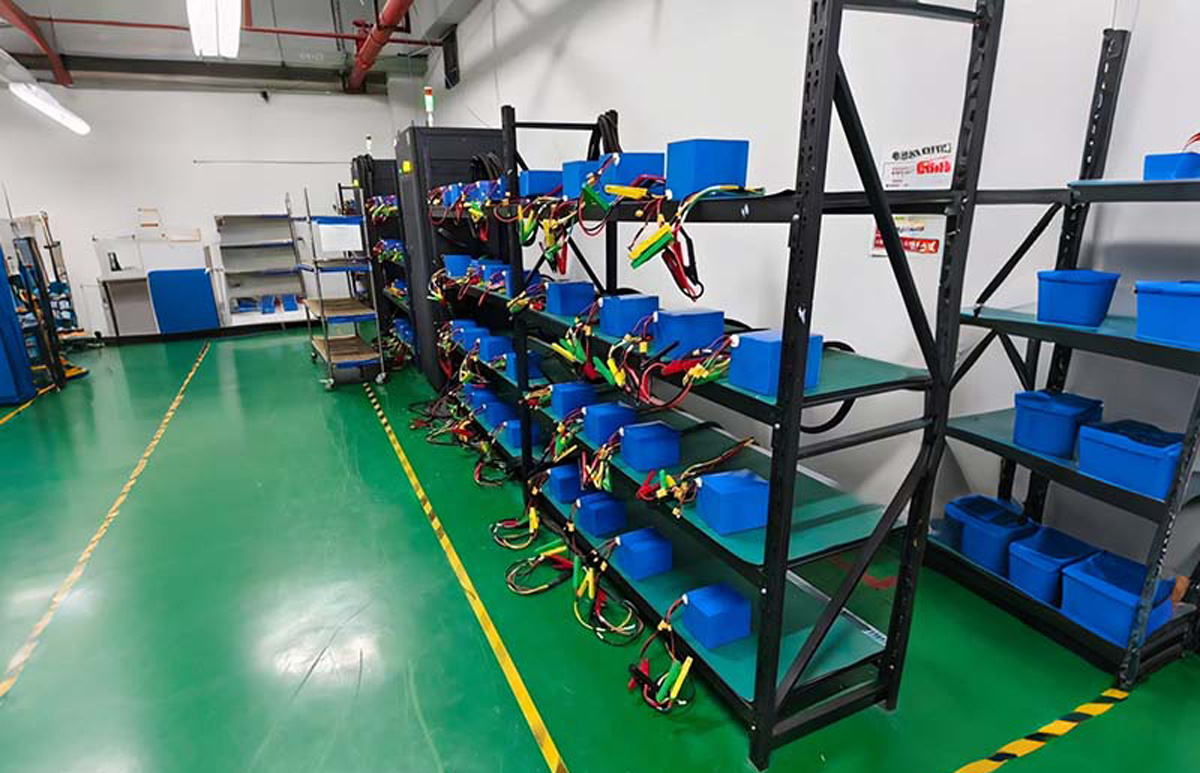
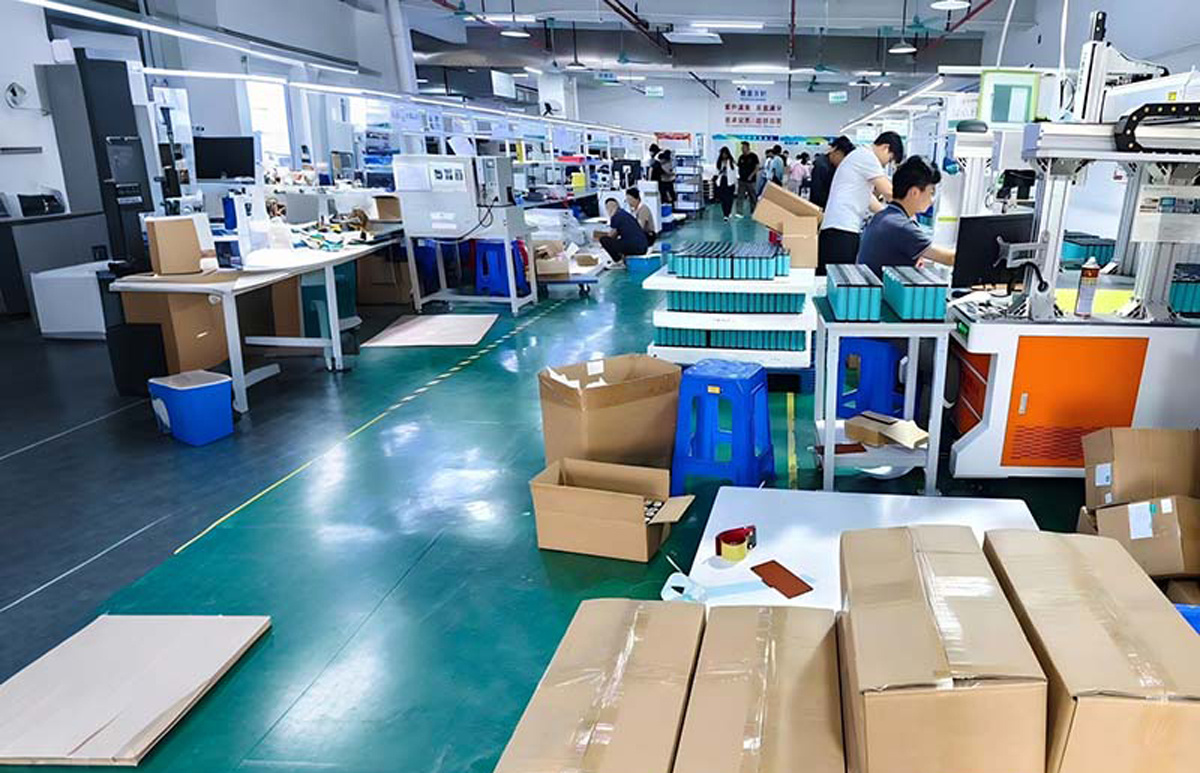
Inside our advanced manufacturing facility where high-precision engineering meets strict quality control.
As a professional battery manufacturer, our factory has upgraded a fully automated production line tailored to battery manufacturing, covering the entire process from material input to finished product delivery.
We’re equipped with industry-leading intelligent equipment: automatic cell sorting machines, robotic spot-welding systems, and PCB precision processing workshops—these cut manual intervention by 80% while boosting production efficiency by 60%.
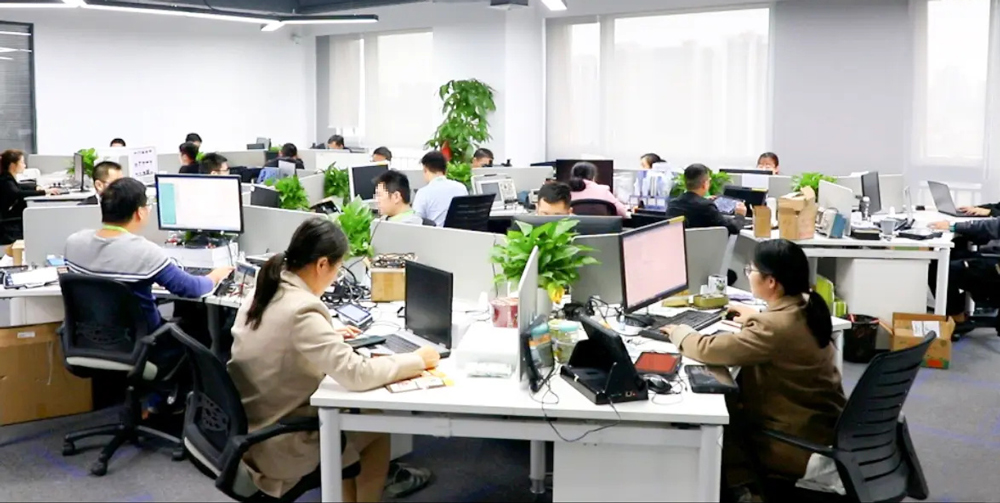
Our 70+ professional team (including automation engineers, quality inspectors, and logistics specialists) monitors every link: from incoming material verification, real-time tracking of cell sorting accuracy, to 100% coverage of aging tests and finished product performance detection.
Our team is a professional and experienced group that has been deeply involved in the battery industry for over a decade. We have accumulated profound industry knowledge and are always committed to technological innovation and quality improvement. We have built a strong and integrated capability covering R&D, production, marketing and after-sales service, making us a reliable partner in the battery field.
In terms of R&D and production, we have a team of senior engineers and technical experts with rich experience in battery technology research and product development. Equipped with advanced production equipment and strict quality control systems, we can independently complete the whole process from product design, technology research to mass production, ensuring stable product quality and high performance that meet market demands.
In marketing and after-sales service, we have a professional team with keen market insight and efficient execution. We have established a comprehensive marketing network to accurately grasp market trends and provide customized solutions for customers. Meanwhile, our after-sales team responds quickly to customer needs, providing timely technical support and service guarantee, winning wide recognition and trust from customers. With our all-round strength, we are committed to promoting the development of the battery industry and creating greater value for our partners.
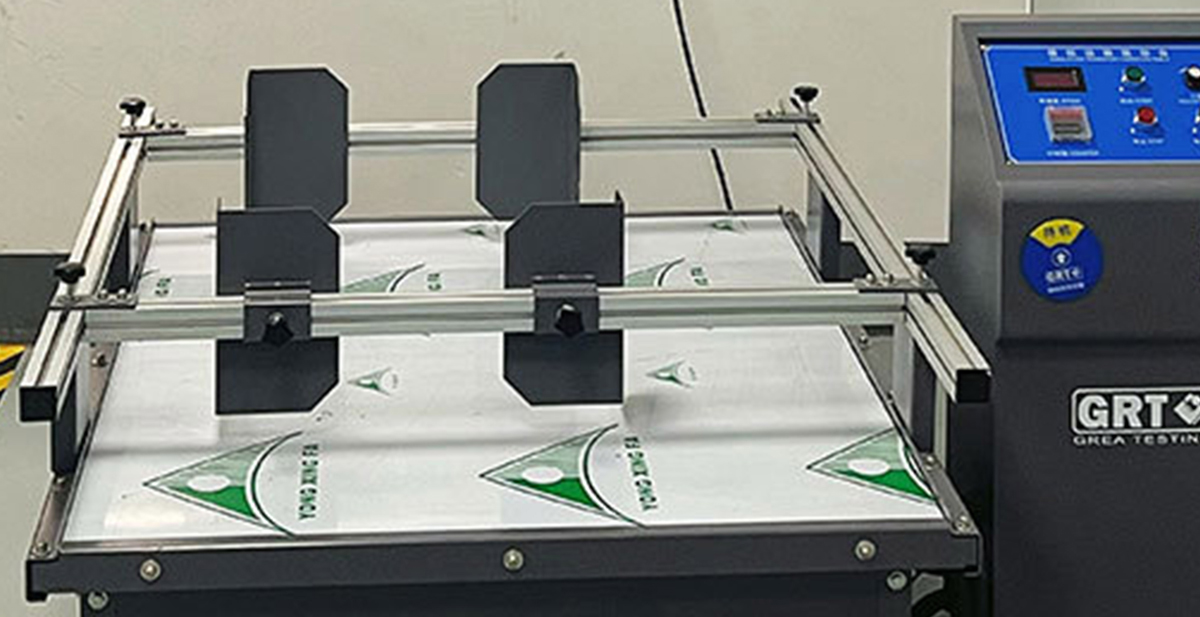
API 6D, API 607, CE, ISO9001, ISO14001, ISO18001, TS. (If you need our certificates, please contact us)
MSDS
FCC
Quality Approved
PSE
UN 38.3
DGM
CE
RoHS
Review our full range of industrial and consumer replacement batteries, built to international standards with rigorous performance testing.