Leave Your Message
Explore our fast-shipping, high-performance battery replacements engineered to match OEM specifications for major American retail and warehousing handheld devices.
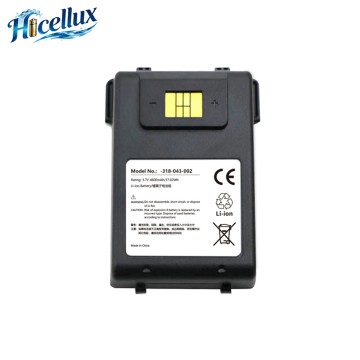 US Logistics Hub 3.7V 4600mAh Intermec CN70, CN70e, CN75, Replacement Battery
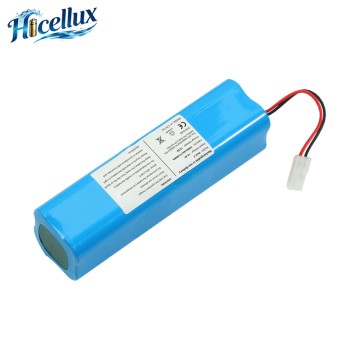 US Facility Care 14.4V 5200mAh Tefal Vacuum Cleaner Ver2 Replacement Battery
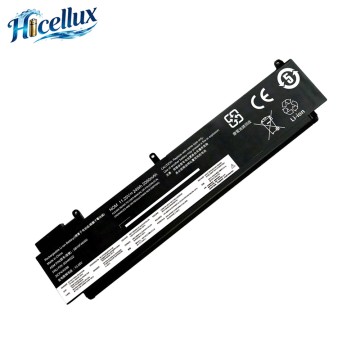 US Corporate Fleet 11.25V 2090mAh Lenovo 01AV406 00HW024 Replacement Battery
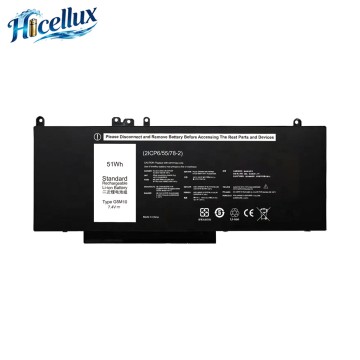 US Professional Workstation 7.4V 6892mAh Dell 51WH Replacement Battery
In the fast-paced United States retail and logistics market, efficiency is the baseline for survival. From massive fulfillment centers in the Inland Empire of California to regional distribution hubs in Dallas-Fort Worth and Chicago, the reliance on handheld Personal Digital Assistants (PDAs), enterprise barcode scanners, and mobile computers has never been higher. These rugged mobile units serve as the nervous system of modern commerce, tracking inventory, processing point-of-sale (POS) transactions, managing last-mile deliveries, and ensuring omnichannel accuracy.
However, the operational efficiency of these devices is entirely dependent on their power source. A dead PDA battery halts a worker's shift, delays shipping schedules, and directly results in lost revenue. Consequently, US businesses are shifting away from unreliable third-party power cells toward certified, high-capacity retail PDA battery manufacturers capable of delivering long-lasting, safe, and OEM-compatible energy solutions.
With the exponential growth of e-commerce and Buy Online, Pick Up In Store (BOPIS) services across the United States, retail store associates are constantly on their feet, using PDAs to pick items, verify stock levels, and print mobile shipping labels. The demand for continuous uptime requires PDA batteries that can comfortably survive a full 8-to-12-hour shift without degradation. Modern lithium-ion manufacturing processes focus on maximizing energy density while maintaining a lightweight profile, preventing operator fatigue while boosting productivity.
In cold storage facilities and food distribution centers across the Midwest and Northeast regions, standard batteries fail rapidly due to sub-zero temperatures. Advanced battery factories utilize specialized low-temperature electrolyte formulations and integrated heating circuits. This ensures that barcode scanners and thermal printers operate reliably at temperatures as low as -20°C, maintaining uninterrupted supply chain operations.
We provide one-on-one customized services and cost-effective solutions for our clients.
Compared to our competitors, we offer faster shipping times and more flexible delivery options.
Our company is committed to helping customers improve efficiency and increase profits.
We welcome your inquiries and look forward to building long-term, mutually beneficial partnerships with clients worldwide.


The industrial landscape in America is undergoing rapid digitalization. To keep up with these technological advancements, battery manufacturers are integrating smart technologies directly into the battery pack. Below are the key trends driving the replacement battery market:
US warehouse operators demand real-time diagnostics. Modern PDA batteries are equipped with intelligent BMS that monitor health status, track charge cycles, and prevent overcharging or thermal runaway. This allows IT managers to proactively replace batteries before they fail in the field.
Safety is non-negotiable in the US market. Batteries must meet strict certifications such as UL 2054 (Standard for Household and Commercial Batteries), IEEE 1725, and UN 38.3 for transport safety. Compliance ensures liability protection and safe daily usage in busy distribution centers.
To reduce downtime, retail warehouses require fast-charging solutions that do not compromise battery longevity. Advanced lithium-polymer cells support high-current charging, reaching 80% capacity within an hour, while extending the overall cycle life to over 500 charge-discharge cycles.
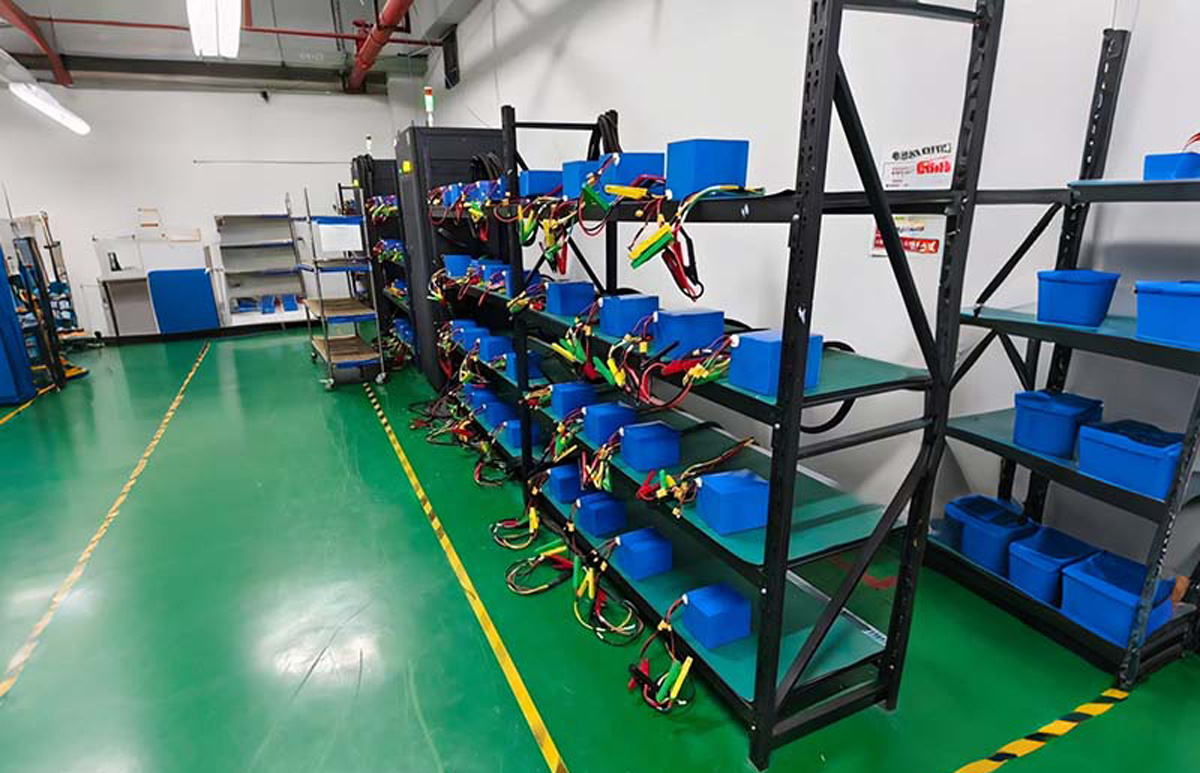
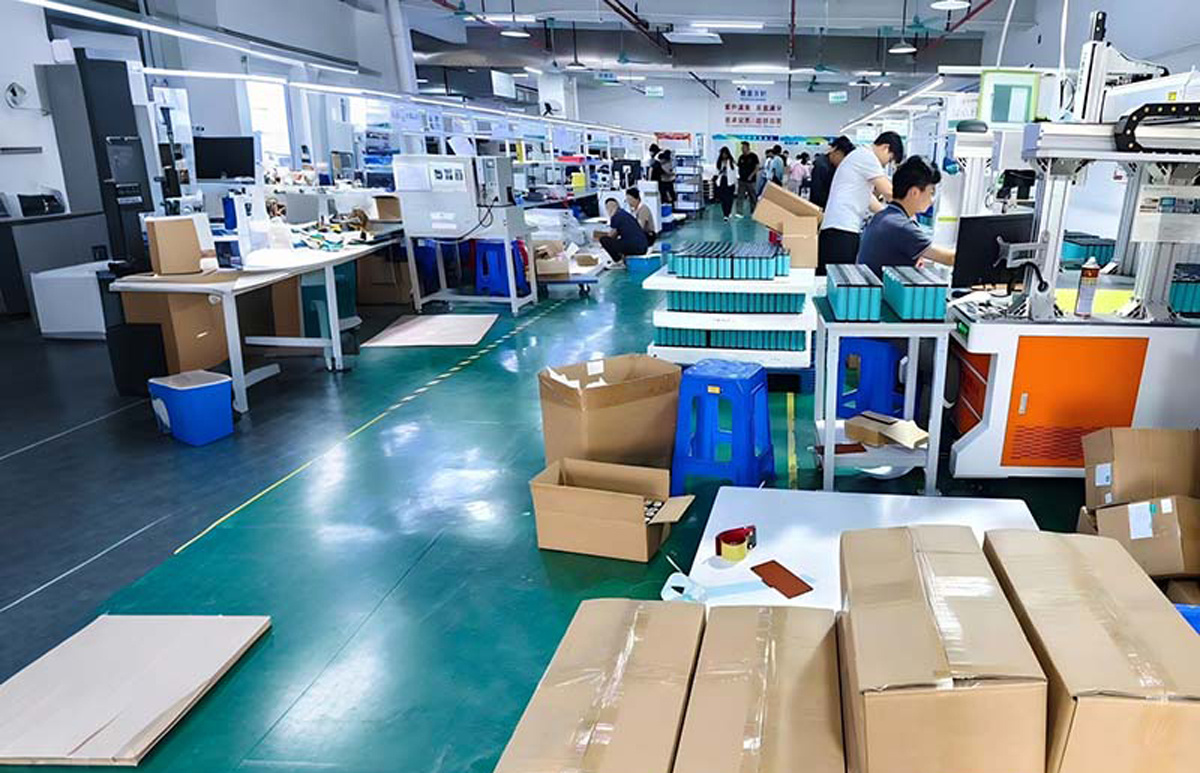
As a professional battery manufacturer, our factory has upgraded a fully automated production line tailored to battery manufacturing, covering the entire process from material input to finished product delivery.
We’re equipped with industry-leading intelligent equipment: automatic cell sorting machines, robotic spot-welding systems, and PCB precision processing workshops—these cut manual intervention by 80% while boosting production efficiency by 60%.
Our 70+ professional team (including automation engineers, quality inspectors, and logistics specialists) monitors every link: from incoming material verification, real-time tracking of cell sorting accuracy, to 100% coverage of aging tests and finished product performance detection.
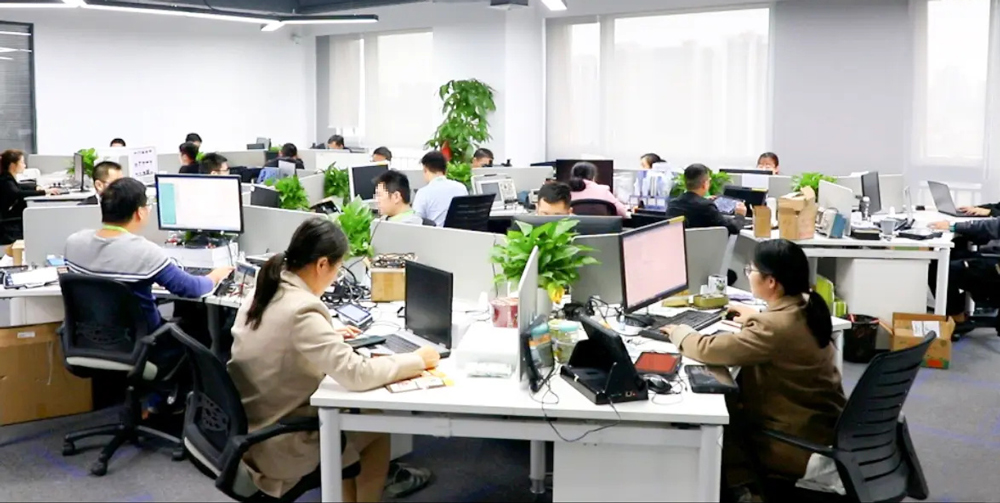
Our team is a professional and experienced group that has been deeply involved in the battery industry for over a decade. We have accumulated profound industry knowledge and are always committed to technological innovation and quality improvement. We have built a strong and integrated capability covering R&D, production, marketing and after-sales service, making us a reliable partner in the battery field.
In terms of R&D and production, we have a team of senior engineers and technical experts with rich experience in battery technology research and product development. Equipped with advanced production equipment and strict quality control systems, we can independently complete the whole process from product design, technology research to mass production, ensuring stable product quality and high performance that meet market demands.
In marketing and after-sales service, we have a professional team with keen market insight and efficient execution. We have established a comprehensive marketing network to accurately grasp market trends and provide customized solutions for customers. Meanwhile, our after-sales team responds quickly to customer needs, providing timely technical support and service guarantee, winning wide recognition and trust from customers. With our all-round strength, we are committed to promoting the development of the battery industry and creating greater value for our partners.
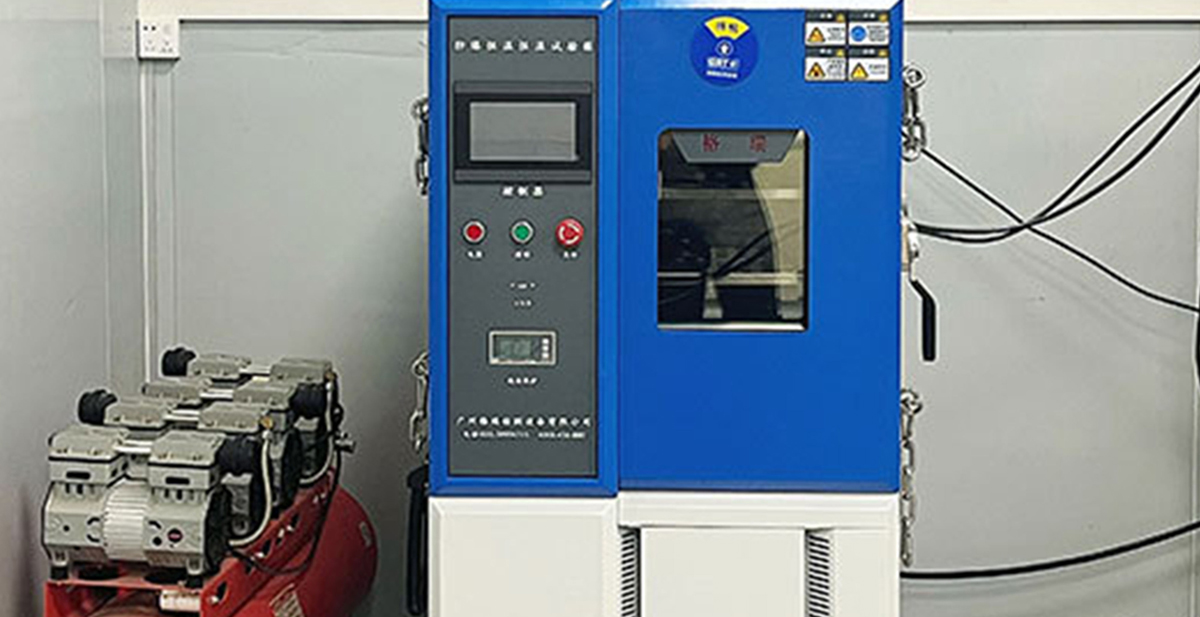
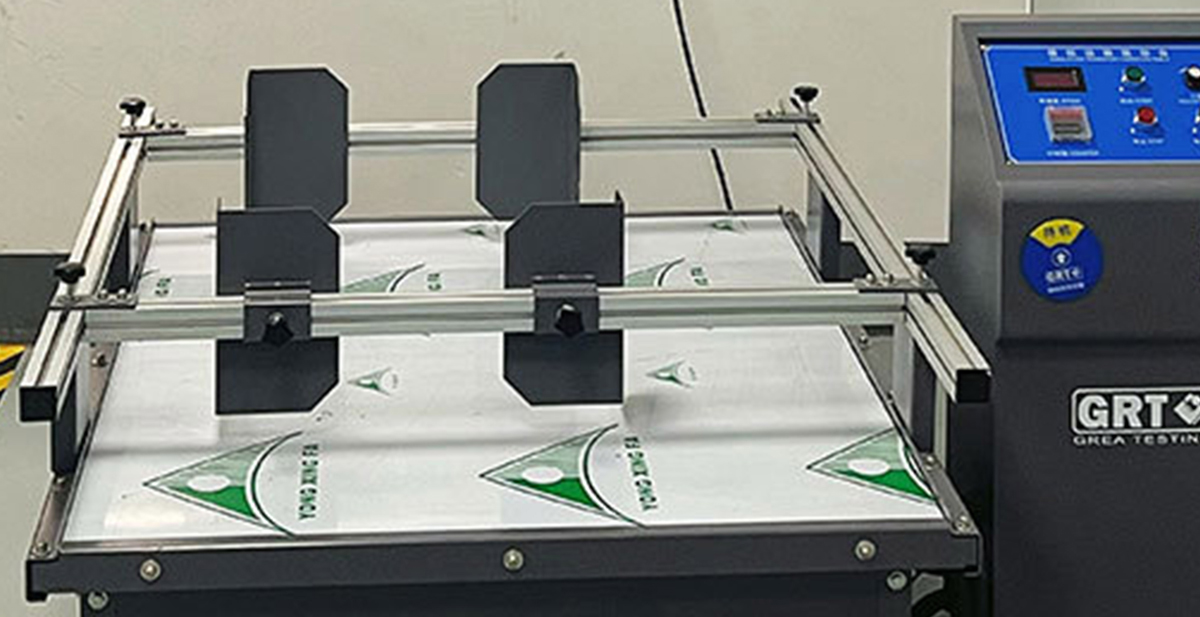
API 6D, API 607, CE, ISO9001, ISO14001, ISO18001, TS. (If you need our certificates, please contact)
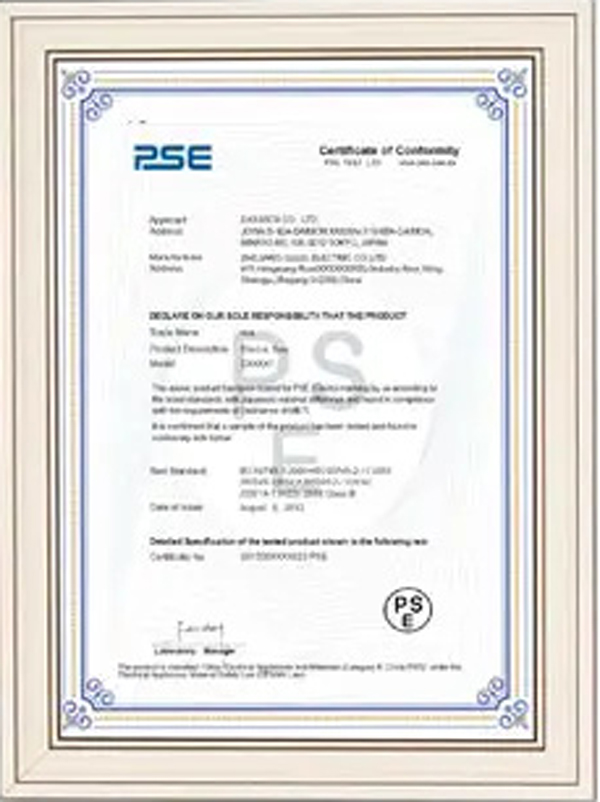
PSE
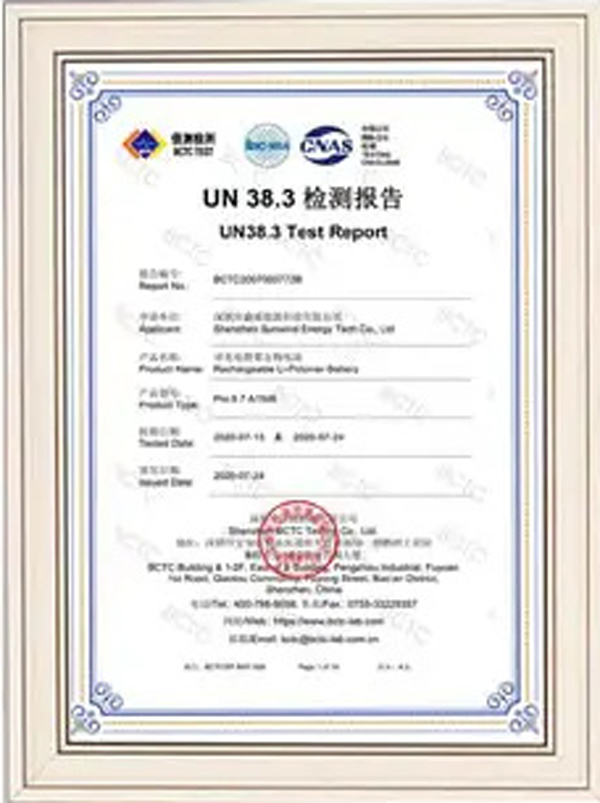
UN 38.3
DGM
CE
RoHS
MSDS
FCC
ISO Standard
Our premium replacement batteries are engineered to perform in various real-world scenarios across the United States. Whether it is in healthcare, retail stores, or distribution centers, we supply reliable power to critical infrastructure.
Drivers for FedEx, UPS, and DHL rely heavily on handheld scanners to log deliveries and capture customer signatures. Operating in varied environmental conditions—from winter blizzards in Chicago to scorching heat in Arizona—requires rugged batteries that resist swelling and maintain charge capacity under stress.
Major retail chains like Walmart and Target equip their associates with mobile computers for real-time inventory management. Our replacement batteries ensure these devices remain operational during high-traffic sales events like Black Friday and Christmas, minimizing checkout delays.
In hospitals and clinics across the US, nursing staff use specialized mobile terminals to scan patient wristbands and administer medication. These devices require clean, reliable power cells that can withstand frequent chemical disinfection and constant duty cycles.
At major maritime ports, such as the Port of Los Angeles and Port of Newark, customs officers use ruggedized mobile computers to inspect container seals and scan barcodes. High-capacity replacement batteries ensure these outdoor operations run smoothly without power failures.
Browse our complete catalog of high-performance replacement batteries. All products are manufactured under strict ISO9001 and CE guidelines, ensuring absolute compatibility and safety.
US Logistics Hub 3.7V 4600mAh Intermec CN70, CN70e, CN75, Replacement Battery
US Facility Care 14.4V 5200mAh Tefal Vacuum Cleaner Ver2 Replacement Battery
US Corporate Fleet 11.25V 2090mAh Lenovo 01AV406 00HW024 Replacement Battery
US Professional Workstation 7.4V 6892mAh Dell 51WH Replacement Battery
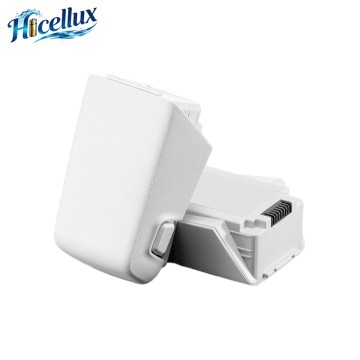 US Commercial Drone Fleet 7.16V 3110mAh DJI Flip Series Replacement Battery
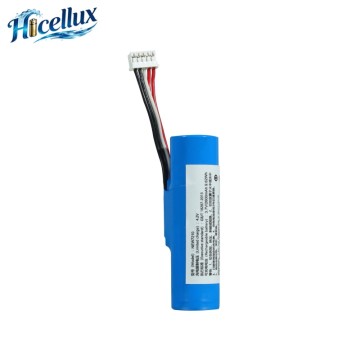 US Retail POS Terminal 3.7V 2600mAh NEWPOS NEW7210 IS588 Replacement Battery
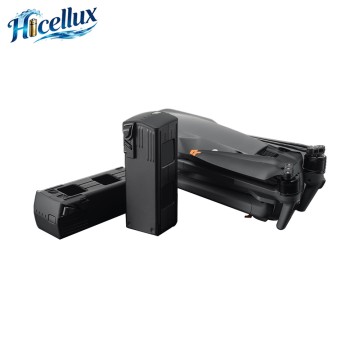 US Mapping & Surveying 15.4V 5000mAh DJI Mavic 3 Series Replacement Battery
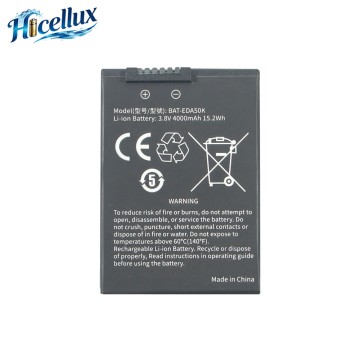 US Retail Warehouse 3.8V 4000mAh Honeywell BAT-EDA50K Replacement Battery