Leave Your Message
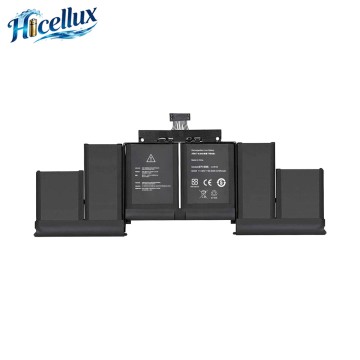
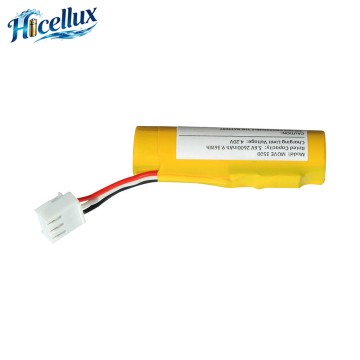
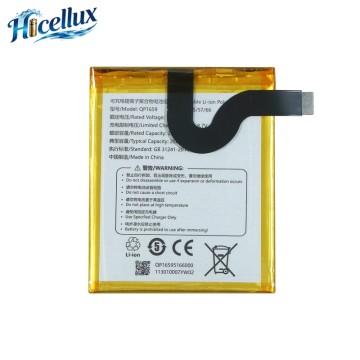
High-efficiency replacement batteries optimized for outdoor operations, tracking terminals, and rugged portable gear.
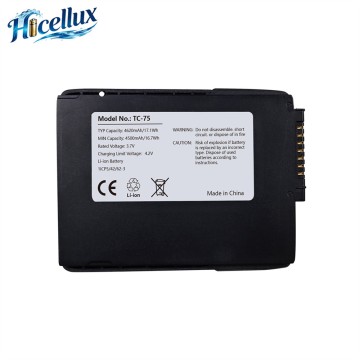
In modern industrial and commercial landscapes, Personal Digital Assistants (PDAs) are no longer confined to climate-controlled warehouse aisles. Today, these devices serve as the central nervous system for field logistics, emergency rescue communication, disaster response coordination, and remote forestry management. The demand for robust, high-performance retail PDA batteries has surged as organizations transition to continuous, off-grid operations where power outlets do not exist.
Whether it is a delivery driver processing a transaction in freezing temperatures or an emergency response team coordinating medical supplies in a post-hurricane zone, the reliability of the device's battery directly influences operational outcome. A failed battery is not just an inconvenience; it represents lost data, halted supply chains, and compromised safety. Consequently, retail PDA batteries have transitioned from simple consumer-grade components into mission-critical power systems built for extreme durability and long-term backup energy storage.
To understand the design requirements of modern retail PDA batteries, one must examine the diverse and demanding environments in which they are deployed:
Delivery personnel frequently move between warm vehicle cabins and sub-zero outdoor environments. Standard lithium-ion batteries suffer severe capacity drops in cold weather. Advanced PDA batteries utilize cold-resistant electrolyte formulations and custom Battery Management Systems (BMS) to ensure consistent power output even in temperatures reaching -20°C, maintaining real-time tracking data and payment processing capability.
When natural disasters strike, power grids fail. First responders rely on rugged hand-held devices to catalog supplies, track survivors, and communicate. In these scenarios, retail PDA batteries act as primary lifelines. Hot-swappable battery designs allow field workers to replace depleted cells without powering down the device, preserving critical operation states and continuous network connectivity.
Surveyors and conservation officers operate in deep wilderness for days or weeks. Their handheld GPS-integrated PDAs must remain active throughout the expedition. High energy density cells, combined with lightweight backup battery packs, ensure that mapping and environmental telemetry can be captured and stored without the anxiety of running out of power.
The global battery market is experiencing rapid technological shifts, driven by the demands of IoT integration, fast charging, and sustainability. Key industry developments include:
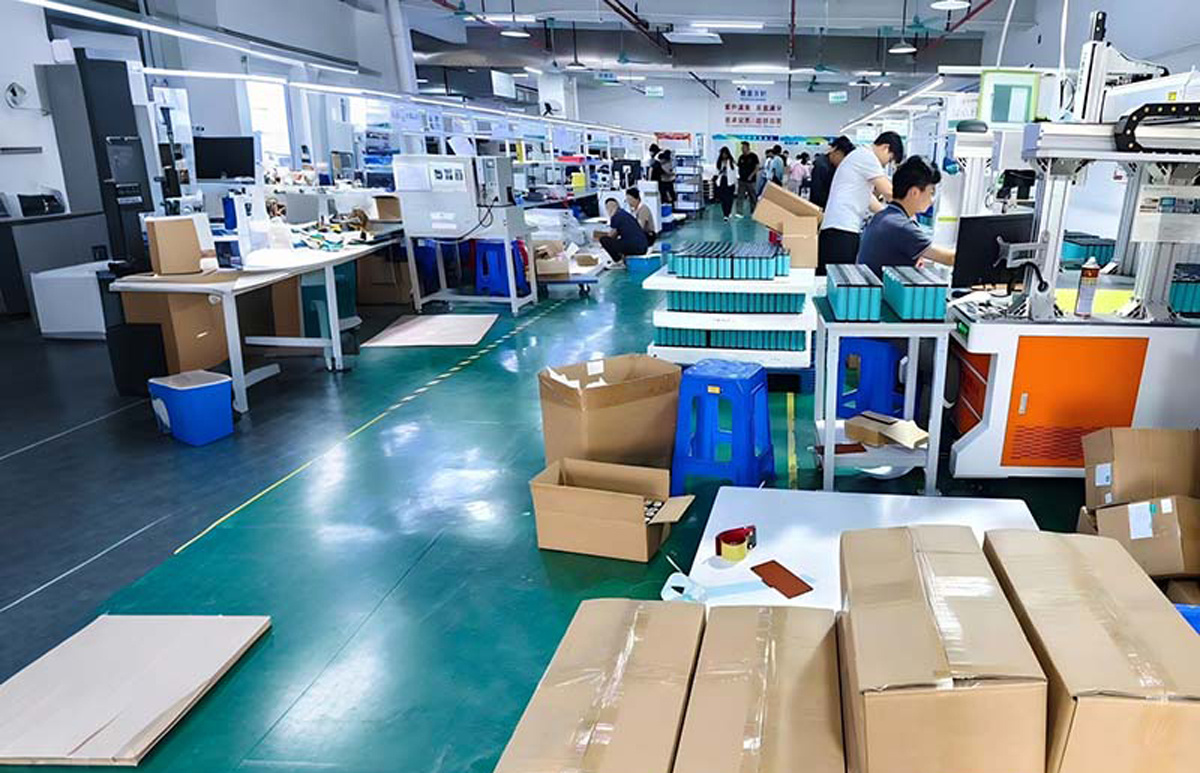
We provide one-on-one customized services and cost-effective solutions for our clients. Compared to our competitors, we offer faster shipping times and more flexible delivery options. Our company is committed to helping customers improve efficiency and increase profits. We welcome your inquiries and look forward to building long-term, mutually beneficial partnerships with clients worldwide.
To lead the global transition toward smart, reliable, and highly efficient portable energy systems.
Empowering businesses with robust battery solutions that maximize device uptime in any environment.
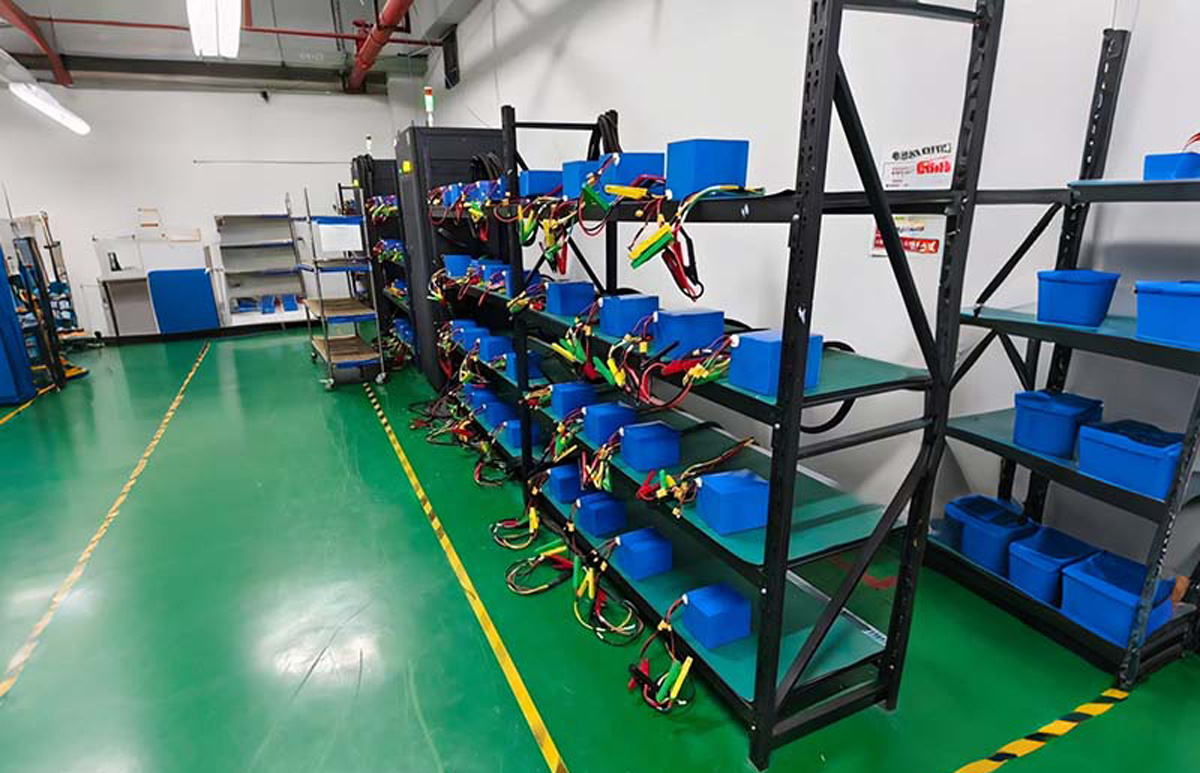
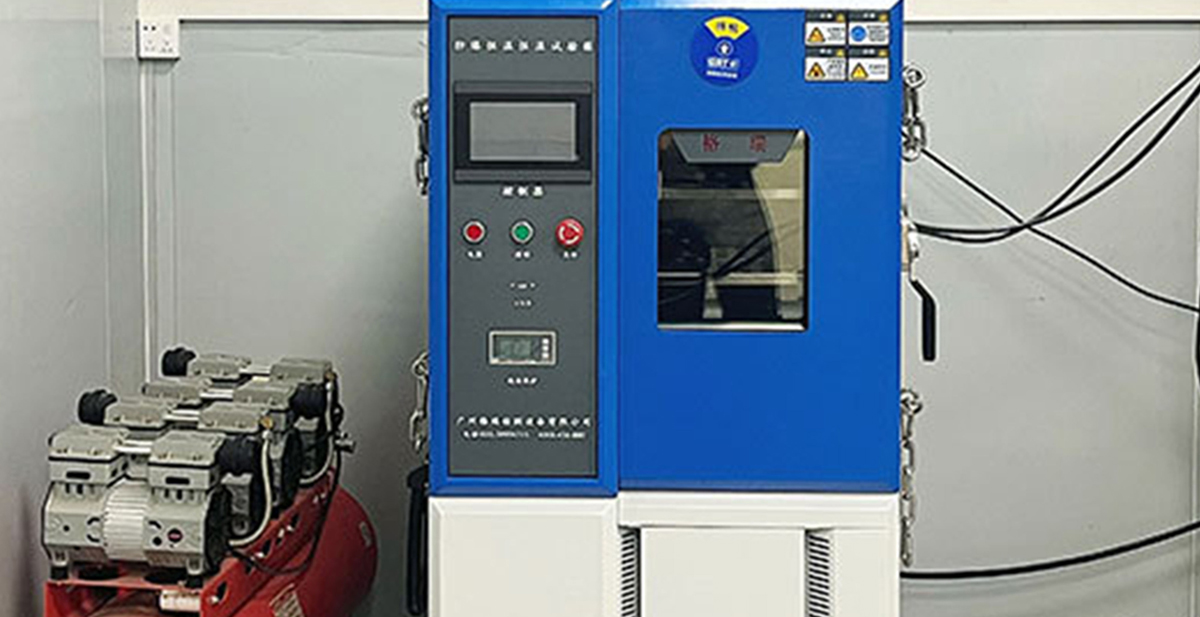
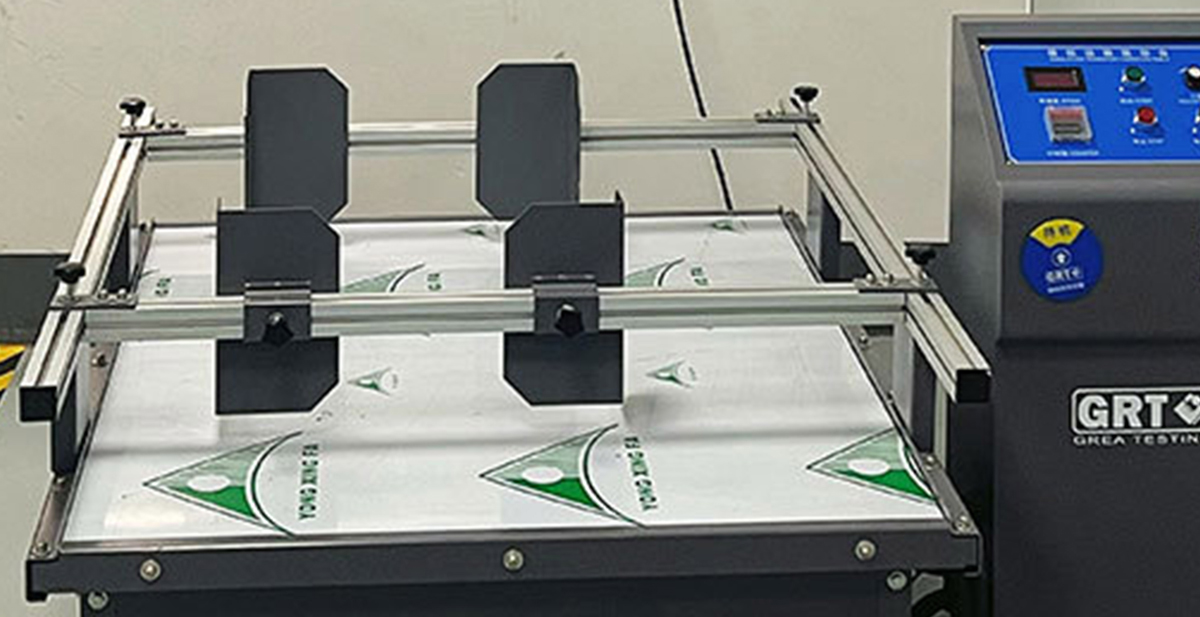
Explore our state-of-the-art production facility where safety, efficiency, and engineering precision converge.
As a professional battery manufacturer, our factory has upgraded a fully automated production line tailored to battery manufacturing, covering the entire process from material input to finished product delivery.
We’re equipped with industry-leading intelligent equipment: automatic cell sorting machines, robotic spot-welding systems, and PCB precision processing workshops—these cut manual intervention by 80% while boosting production efficiency by 60%.
Our 70+ professional team (including automation engineers, quality inspectors, and logistics specialists) monitors every link: from incoming material verification, real-time tracking of cell sorting accuracy, to 100% coverage of aging tests and finished product performance detection.
Our collaborative units work seamlessly to deliver top-tier power products globally.
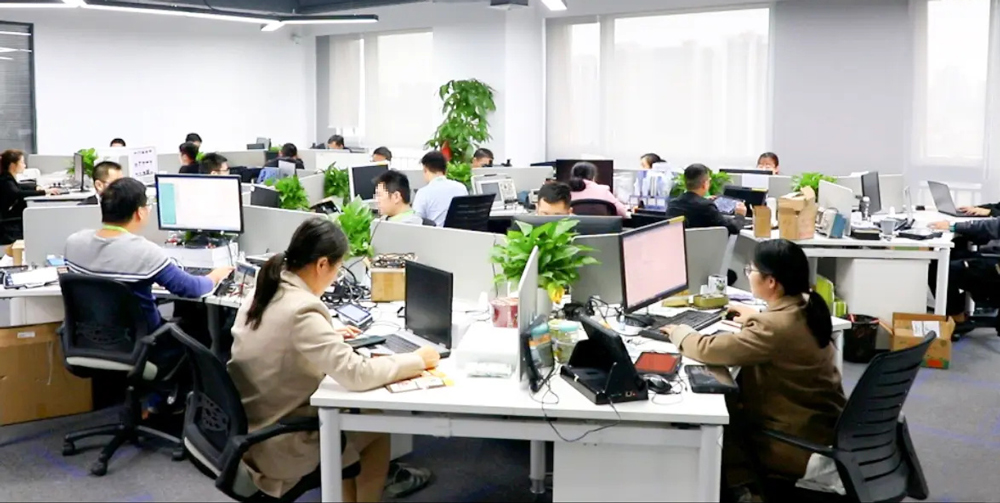
Our team is a professional and experienced group that has been deeply involved in the battery industry for over a decade. We have accumulated profound industry knowledge and are always committed to technological innovation and quality improvement. We have built a strong and integrated capability covering R&D, production, marketing and after-sales service, making us a reliable partner in the battery field.
In terms of R&D and production, we have a team of senior engineers and technical experts with rich experience in battery technology research and product development. Equipped with advanced production equipment and strict quality control systems, we can independently complete the whole process from product design, technology research to mass production, ensuring stable product quality and high performance that meet market demands.
In marketing and after-sales service, we have a professional team with keen market insight and efficient execution. We have established a comprehensive marketing network to accurately grasp market trends and provide customized solutions for customers. Meanwhile, our after-sales team responds quickly to customer needs, providing timely technical support and service guarantee, winning wide recognition and trust from customers. With our all-round strength, we are committed to promoting the development of the battery industry and creating greater value for our partners.
API 6D, API 607, CE, ISO9001, ISO14001, ISO18001, TS. (If you need our certificates, please contact us for official copies)
PSE
UN 38.3
DGM
CE
RoHS
MSDS
FCC
ISO Certified
Browse our entire catalog of high-capacity replacement batteries engineered to support commercial, retail, and outdoor operations.